Control Plan Software for Manufacturing
The control plan is the document the shop floor actually works to. It should be the same operations as the process flow and the same controls as the PFMEA — because in a good quality system those are one decision, recorded once.
Already have an account? Login
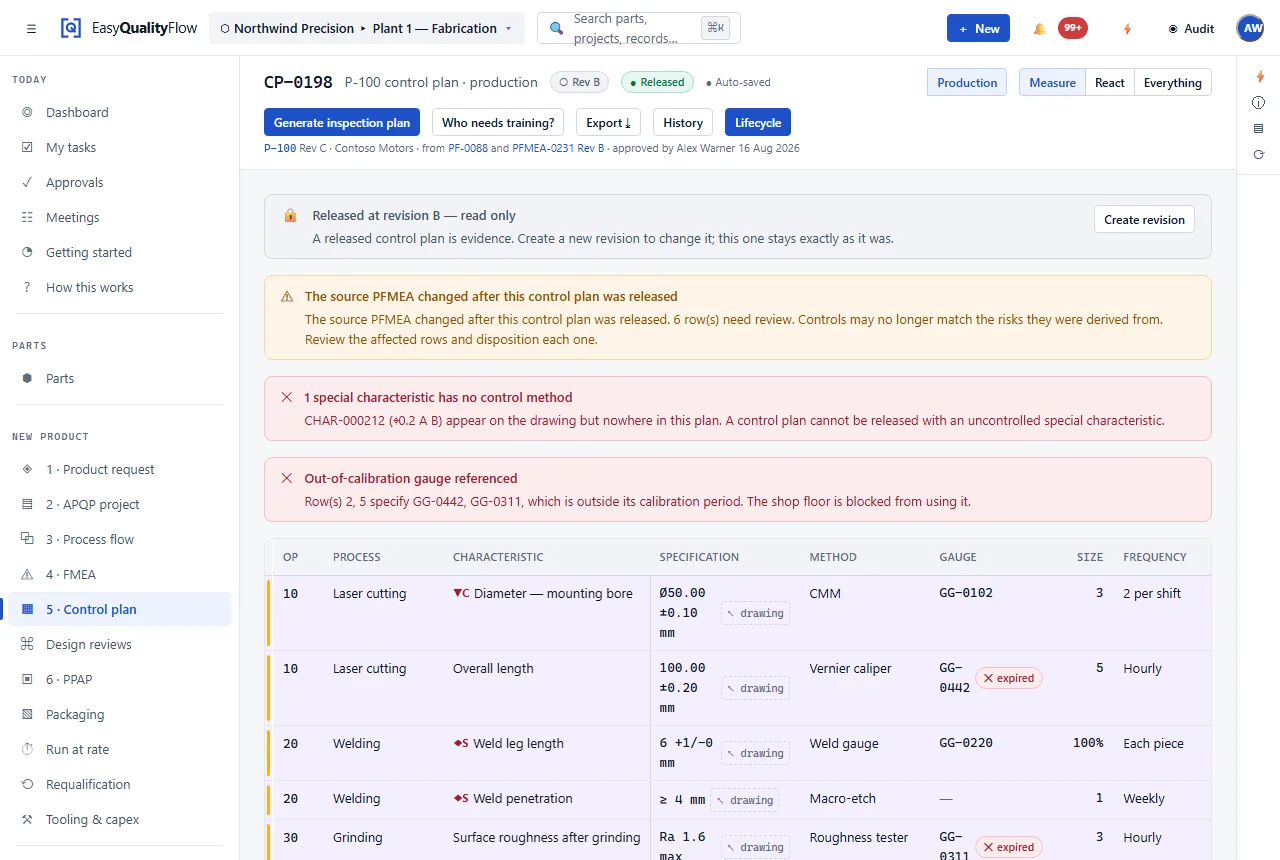
Three documents describing one process.
Process flow, PFMEA and control plan are, in most quality departments, three separate files maintained by the same person under time pressure. They agree on the day they are created. After the first process change they agree less, and nobody finds out until an audit walks the line with the control plan in hand.
Holding all three on one operation list makes them structurally consistent. A characteristic is created once on the part, appears at the operation that produces it, gets analysed in the PFMEA, and is controlled in the control plan — the same characteristic each time, not four copies of its name.
One operation list
Process flow, PFMEA and control plan built on the same operations.
Characteristics, referenced
A characteristic comes from the part record and is referenced, never re-typed.
Specification and method
Nominal, tolerance, measurement method, sample size and frequency.
Special characteristic classes
Critical and significant classification carried down from design.
Reaction plan
What happens when a control fails, recorded with the control.
Revision control
Revisions and states, so the plan on the line is the plan that was approved.
Two stages, one spine.
Process defines the operations. The control plan says what is verified at each of them. Inspection then records results against exactly those controls, which is what makes the results evidence rather than numbers.
- Operations shared with the process flow and PFMEA
- Characteristics referenced from the part record
- Specification, method, sample size and frequency
- Critical and significant classification carried down
- Reaction plan held with the control
- Controls carried into the inspection plan
Connected capabilities
Every one of these works on the same record. That is the point of the platform.
Questions about Control plan software
What is a control plan?
How is a control plan different from a process flow?
Where do the control plan characteristics come from?
Can we have different control plans for prototype, pre-launch and production?
Does the control plan feed inspection?
One operation list. Three documents that agree.
Bring APQP, FMEA, PPAP, process flow, control plans, inspection and SPC into one connected platform.
Questions? support@easyqualityflow.com